Can approved screw samples hold batch‑consistency for high‑volume assembly lines?
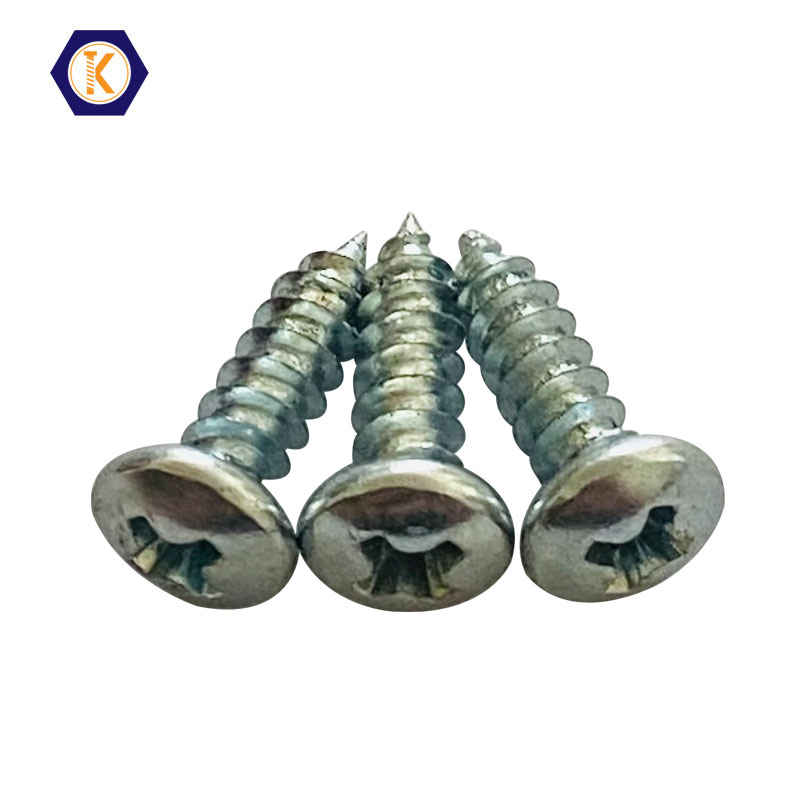
KOIN builds multi‑layer pre‑qualification workflows for Flat Philip Head Wood Screw Zinc Plated, combining thread‑tool wear‑cycle monitoring, assembly‑line‑simulated torque endurance testing and lot‑wise plating‑thickness spot‑verification, unearthing sample‑concealed batch‑variability risks well before bulk‑fastener shipments go to furniture OEM and hardware‑distributor partners.
1. Thread‑rolling tool wear‑cycle tracking mitigates progressive thread‑profile deviation
Qualification‑samples are produced using brand‑new, sharp thread‑rolling dies. Over millions‑of‑pieces serial‑production runs, rolling dies sustain gradual abrasive wear. Thread root radius, pitch contour and effective major‑diameter drift slowly. Visual inspection may overlook minor profile changes, yet altered thread geometry modifies tapping resistance and holding‑power when driven into wood or thin metal substrates. Static sample acceptance cannot predict tool‑wear‑related batch‑to‑batch shift. KOIN implements fixed output‑count trigger thresholds for thread‑rolling‑die refurbishment. Periodic cross‑section thread‑profile sampling validates geometry stability over full production cycles, lowering sporadic bad‑thread‑related assembly‑line stoppage risks for automated furniture‑manufacturing lines.
2. Simulated automated‑assembly torque‑cycling uncovers drive‑recess cam‑out tendency
Sample‑evaluation usually applies careful manual screwdriver operation. Real‑world mass‑production utilises high‑torque pneumatic or electric auto‑feed drivers. Minor recess‑geometry variation combined with slight surface‑plating build‑up amplifies cam‑out risk under repeated high‑speed driving cycles. Even screws passing static dimension‑check can strip phillips recess heads on‑assembly‑shop floors. KOIN runs accelerated auto‑driver torque‑cycling lab‑simulation replicating typical furniture‑plant assembly‑parameters. Post‑cycling recess‑damage assessment filters borderline geometry‑plating combinations, stabilising drive‑performance for high‑volume automated‑fastening workflows.
3. Lot‑by‑lot plating‑thickness mapping avoids uneven corrosion‑resistance drift
Approval‑samples receive optimised electro‑plating bath settings. During extended continuous plating campaigns, bath‑chemistry, current‑density and part‑rack‑loading conditions shift. Local zinc‑thickness variance arises over screw‑threads, recess‑cavities and head‑under‑fillet zones. Average salt‑spray test result can still pass specification while local thin‑zinc spots create early rust initiation points in humid end‑use environments. Single‑sample salt‑spray reports are insufficient for judging serial‑lot real‑world anti‑corrosion performance. KOIN executes multi‑position XRF plating‑thickness spot‑checks across each completed production lot, verifying minimum zinc‑thickness at hard‑to‑plate critical zones, mitigating field‑premature‑rust complaint risks for furniture exposed to variable‑humidity conditions.
4. Heat‑treatment quenching‑batch auditing controls hardness‑spread across serial‑output
Sample‑phase heat‑treatment achieves tightly‑controlled surface‑and‑core hardness matching drawing‑requirements. In large‑batch continuous‑furnace operations, load‑position variation, furnace‑atmosphere fluctuation and quenching‑oil condition generate hardness‑spread within one single shipment lot. Some individual screws become overly brittle while others show insufficient tapping‑hardness. Both conditions create field‑failure: brittle units fracture under driving‑torque; soft screws experience thread‑deformation during self‑tapping installation. KOIN deploys multi‑specimen hardness‑sampling per furnace‑batch covering different tray‑positions. Hardness‑spread acceptance‑limits reduce mixed‑property‑batch outflow to OEM furniture‑assembly customers.
5. Hydrogen‑embrittlement risk assessment for post‑plating high‑strength screw lots
Zinc electro‑plating introduces inherent hydrogen‑absorption risk for carbon‑steel fasteners. Qualification‑samples commonly undergo full de‑hydrogen baking process. In busy high‑volume‑production, de‑bake cycle‑time or temperature may drift under production‑schedule pressure. Latent hydrogen‑embrittlement creates delayed brittle‑fracture; screws survive installation and crack hours or weeks after fastening under static pre‑load stress. This failure‑mode cannot be spotted through routine dimensional‑or‑hardness spot‑check. KOIN implements mandatory post‑plating baking‑process traceability plus periodic sustained‑load slow‑fracture verification for every high‑strength screw lot, minimising delayed‑in‑service‑cracking liability for finished‑furniture OEM projects.
6. Consolidated fastener‑lot traceability‑dossiers simplify third‑party hardware‑audit workflows
International furniture‑brand incoming‑QA and retail‑chain supplier‑audits demand aggregated manufacturing records: thread‑tool‑change logs, plating‑thickness test‑logs, furnace‑heat‑treatment‑batch‑reports and hydrogen‑de‑bake‑process evidence. Isolated prototype‑sample‑certificates possess zero audit‑validity for million‑piece bulk shipments. Without lot‑specific English‑language traceability‑archives, hardware‑batches risk incoming‑QA rejection and hold‑up furniture‑production‑schedules. KOIN compiles unified project‑oriented lot‑tied documentation‑packages for pan‑phillips‑head zinc‑plated‑screw orders. Complete traceable archives remove documentation‑gap‑driven assembly‑line‑delay risks for cross‑border furniture‑OEM and hardware‑distributor clients worldwide.